There is an environmental problem hiding in plain sight in every outdoor gear store on earth. Walk the fleece aisle of any well-stocked apparel retailer anywhere in the world, and you will see it. Because the problem is the color black.
Dozens of versions of it hang side by side on racks, each one marginally different from the next in ways that only become visible when you hold two fabric swatches together under bright, direct light. Look closely at a multi-paneled garment constructed entirely from black Polartec fleece made by various outdoor brands for the same season, and the truth becomes apparent: they are simply not the same color.
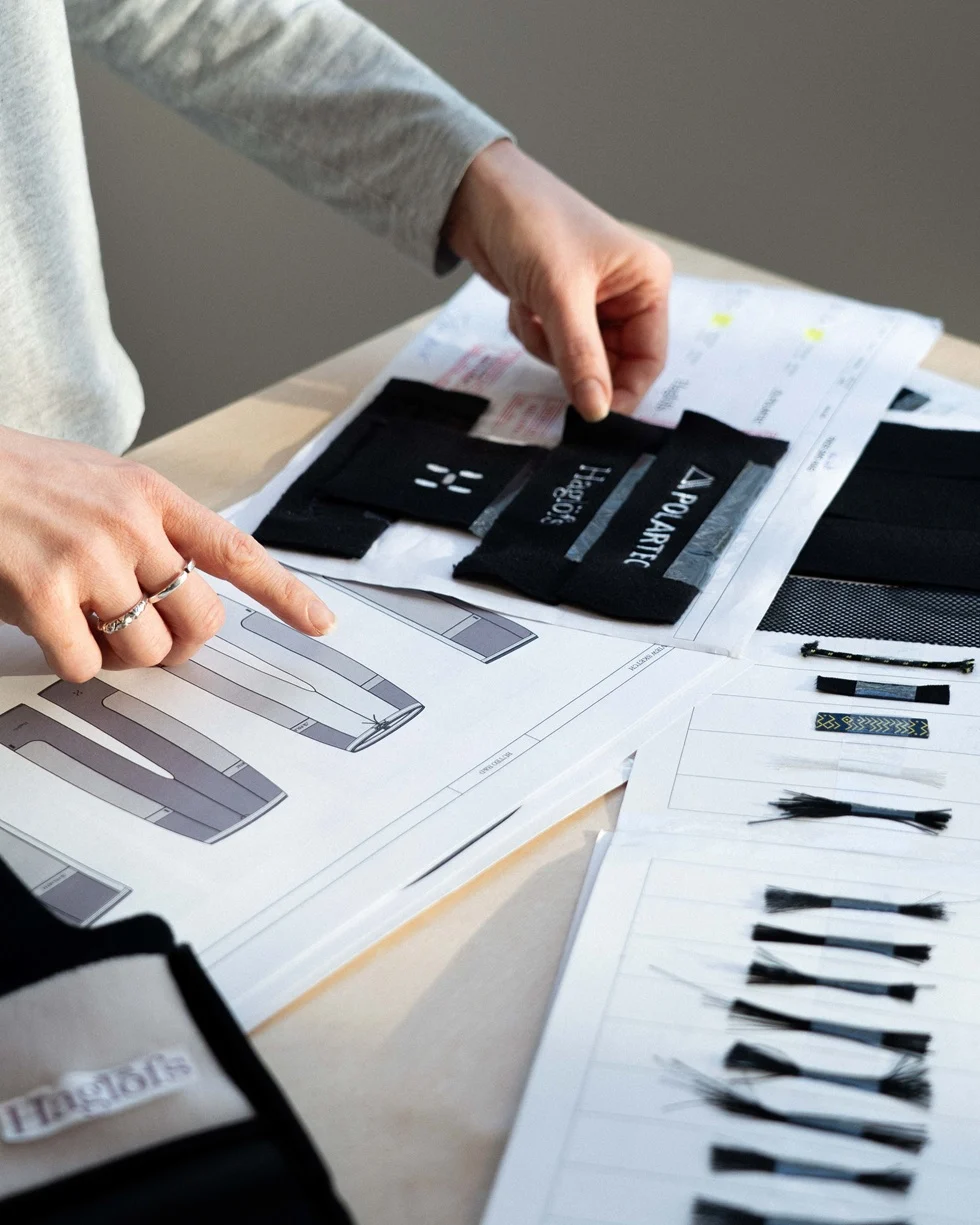
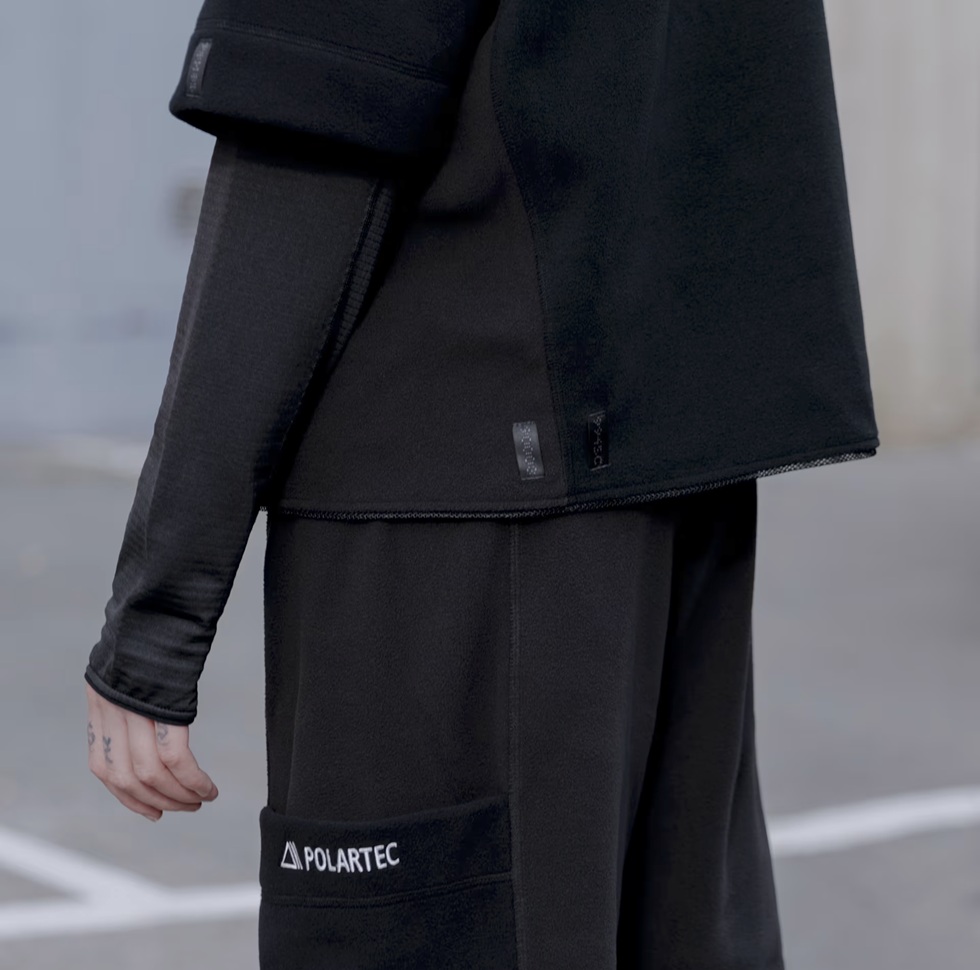
Examine the panels further, and you will notice that each section of the garment carries a woven label stamped with its original color batch number. These batch numbers are there to make a point as plainly as possible: these are distinct, separately commissioned, separately processed, and separately dyed runs of fabric.
The differences between these shades are real enough, but they raise a fundamental question that brands like Haglöfs and Polartec are finally asking: are these microscopic variations important enough to justify the immense resource expenditure required to bring them into existence?
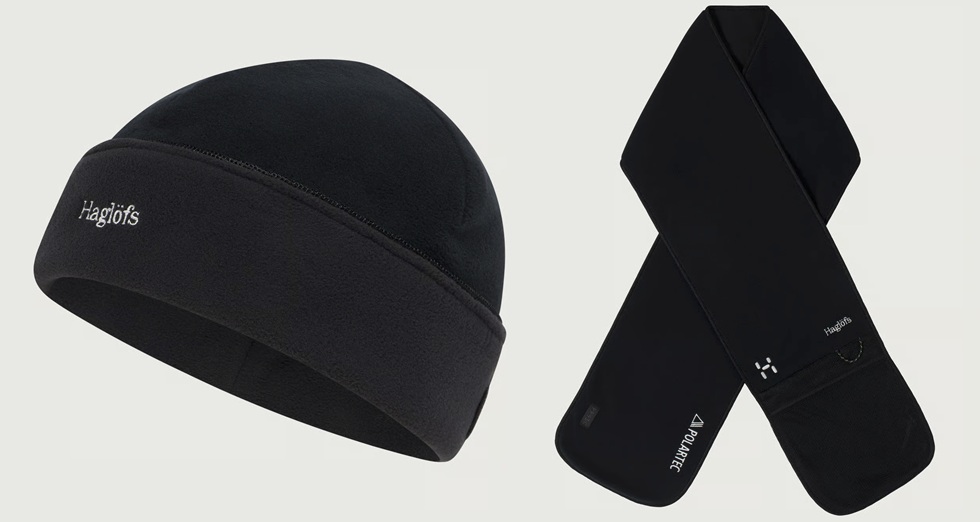
That unique garment is the Black Capsule Project Tee, one piece in a limited collection built by Haglöfs from leftover black Polartec fleece in multiple variations. Alongside a matching beanie, scarf, and pant, these items were created to deliver an unmistakable message to the apparel industry: the outdoor sector is running dozens of separate dye processes, consuming enormous quantities of water and energy, to produce shades of black that are, for all practical purposes, completely identical.
To the retail customer, these minute color differences are entirely invisible. To the brands that manufactured them, however, each shade represents a separate dye batch, a separate chemical formulation, a separate minimum order quantity, and a separate environmental bill that nobody in the corporate supply chain has been adding up.
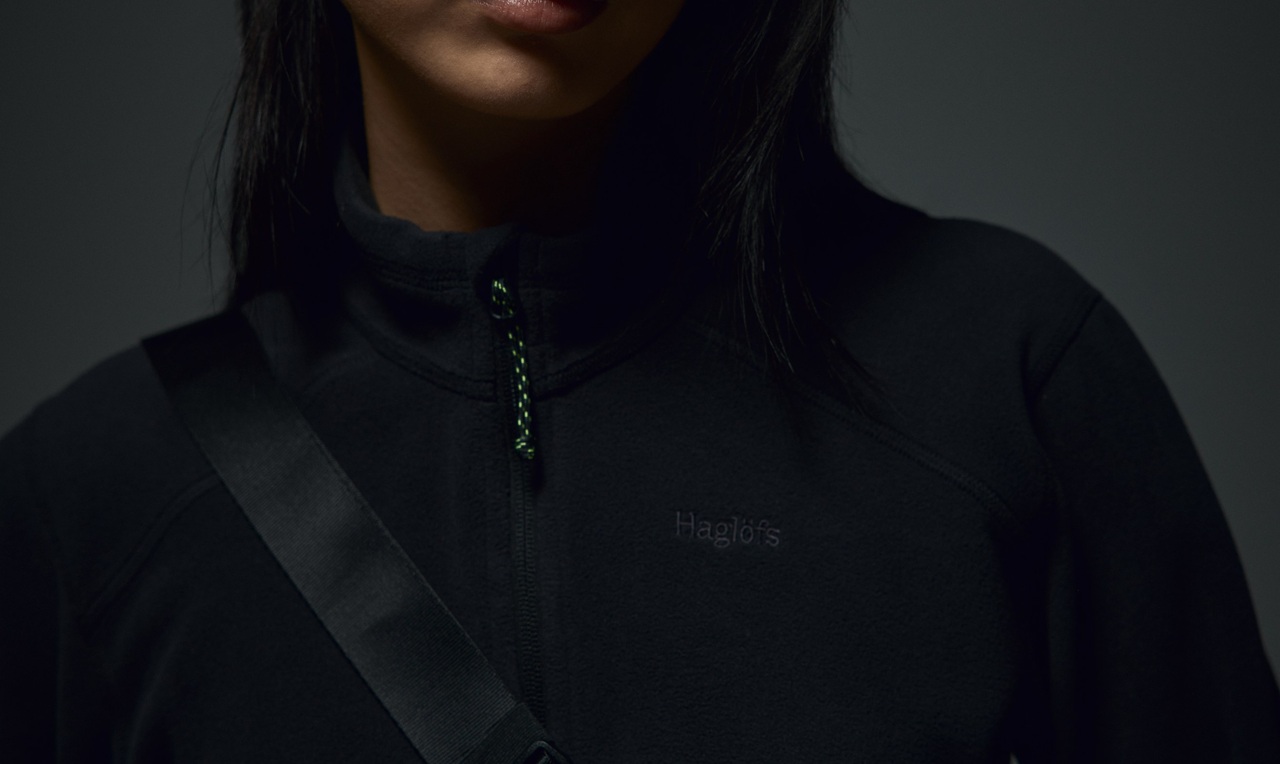
Haglöfs and Polartec started adding it up. What they found is the kind of systemic inefficiency that is simultaneously obvious, highly significant, and almost entirely unaddressed by the broader textile industry. The real question now is whether the rest of the outdoor market is ready to confront it.
The Dye Problem
To understand why the color black presents such a massive environmental hurdle, it is necessary to understand how textile dyeing actually works, particularly when applied to synthetic fibers like the polyester fleece that makes up the bulk of the outdoor industry’s mid-layer clothing offerings.
Polyester does not absorb dye the way natural fibers do. Traditional materials like cotton and wool possess a natural chemical affinity for water-based dyes, allowing manufacturers to color them at relatively low temperatures using modest chemical treatments. Polyester, by contrast, is hydrophobic; it naturally repels water. To force color into synthetic polyester fibers, a completely different class of chemistry is required. Manufacturers must utilize disperse dyes, which are applied at exceptionally high temperatures—typically 130 degrees Celsius or above—under intense pressure inside a hot aqueous bath that forces the dye molecules deep into the polymer structure of the fiber itself.
By its very nature, this industrial process is intensely energy-demanding. Heating large volumes of water to pressure-vessel temperatures and maintaining that thermal state for the duration of a dye cycle is a significant energy ask. Furthermore, black is widely recognized as the most demanding color in the entire textile spectrum. Achieving a deep, consistent, neutral black requires layering multiple disperse dye molecules together, with each individual molecule contributing a specific component to the final shade. This requires more chemistry, additional fixation cycles, vastly increased water usage, and sustained heat.
The global textile industry accounts for roughly 20 percent of worldwide industrial water pollution, with dyeing and finishing operations responsible for the largest single share of that staggering figure. A single kilogram of dyed polyester fabric can require anywhere between 30 and 150 liters of water to process, depending on the specific method utilized, the required depth of the shade, and the operational efficiency of the facility. Black, sitting firmly as the deepest shade in any palette, sits directly at the most resource-demanding end of that range.
Yet the part of this reality that makes the outdoor industry’s version of the problem particularly absurd is that every independent brand is running its own version of this identical process separately, all to produce shades of black that are functionally indistinguishable to the people who wear the garments outdoors.
The Minimum Order Problem
There is also a strict operational reason why this redundancy occurs, and it is rooted directly in the economics of minimum order quantities.
Industrial dye houses operate in batches. To run a dye cycle economically, a facility requires a minimum volume of fabric—typically several hundred kilograms at a minimum, and frequently significantly more. If an outdoor brand wants a proprietary, specific shade of black, it must commission a custom dye recipe, run a dedicated batch, and take delivery of the full minimum order. If the brand’s production volume is high enough, the unit economics work out. If it is not, the company ends up paying a steep premium for a small run of a color that is, for all practical intents and purposes, identical to the one its primary competitor just ordered from the very same dye house.
The resulting system is one in which dozens of competing brands independently commission dozens of marginally different shades of black. Each of these variations requires its own recipe development phase, its own rigorous quality approval process, its own dedicated batch run, and its own heavy chemical and water consumption footprint. The waste inherent in this model does not stem from any single malicious corporate decision; rather, it is the cumulative result of hundreds of rational individual business decisions that, when aggregated together, produce a profoundly irrational collective outcome.
These are precisely the systemic supply chain problems that the new Standard Issue Black initiative is engineered to solve.
The Black Capsule
Before Haglöfs introduced a commercial mass-market product utilizing this new philosophy, the company launched its public argument through conceptual design.
The Black Capsule collection—featuring a limited run of the Project Tee, a beanie, a scarf, and a pair of pants—served as a direct piece of visual sustainability communication. Each garment in the capsule was assembled from three distinct shades of leftover black Polartec fleece, stitched together into a single, cohesive piece to highlight the unintended variation hiding within standard manufacturing streams.
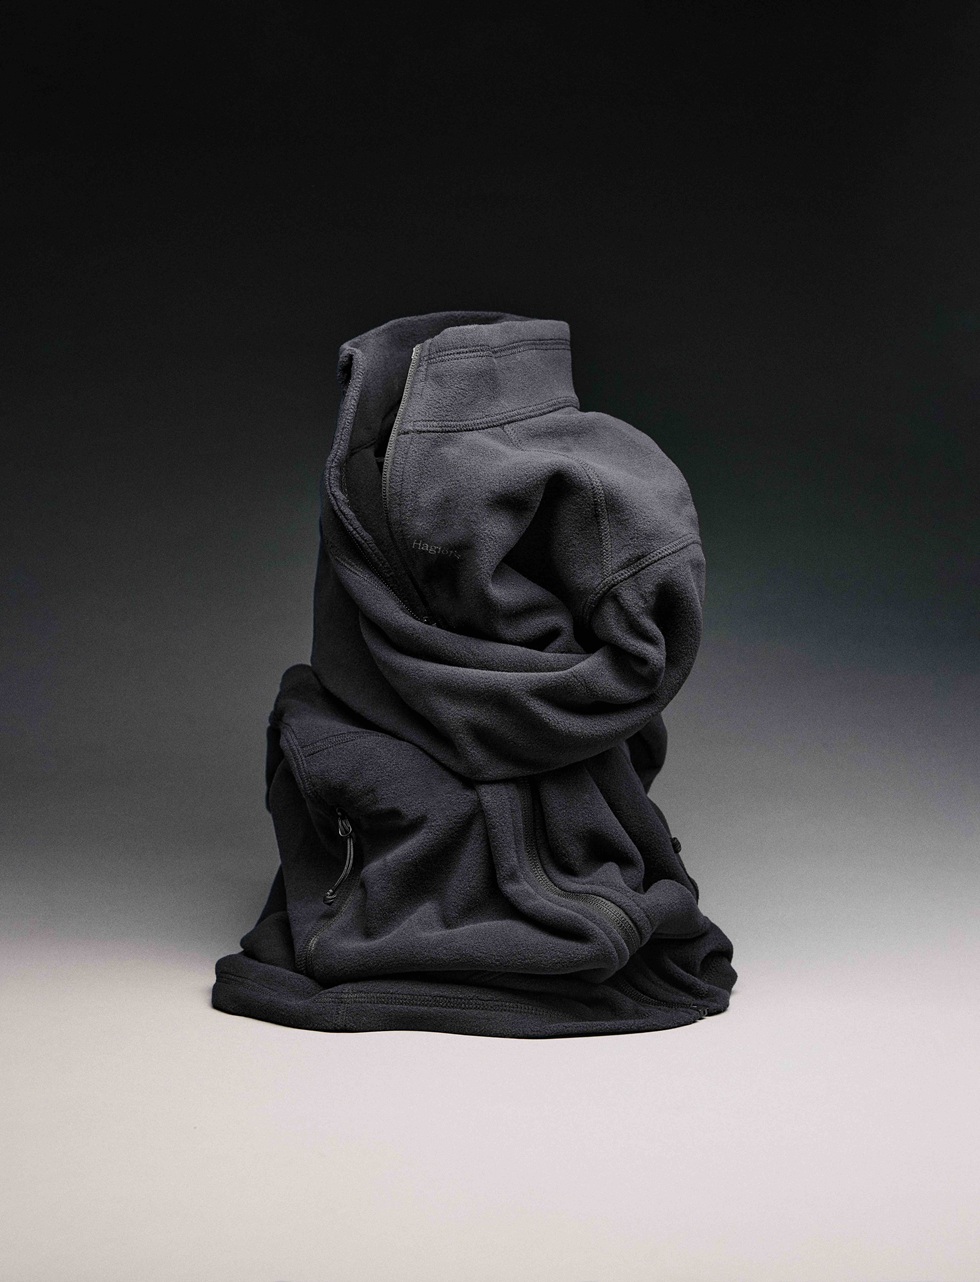
Every single pattern piece on every garment in the Black Capsule carries a woven label stamped with its original color batch number. This number tells the observer exactly which industrial dye run produced that specific panel, and by extension, exactly how many separate, resource-intensive dye runs were required to manufacture the minor visual variations held in the consumer’s hands.
A Universal Black for the Industry
The solution that naturally follows from the experimental Black Capsule is, in its core concept, almost aggressively simple. Haglöfs and Polartec mutually agreed upon a single, optimized shade of black, had it dyed at massive industrial scale by Polartec as part of their standard production workflow, and made it openly available to the entire outdoor apparel industry. There is no proprietary lock-in, no restrictive licensing fee, and no competitive advantage withheld from the market. It is one universal black, shared freely with any brand that wants it and understands its systemic value.
The environmental arithmetic supporting this move flows directly from standard industrial economics of scale. When a manufacturer consolidates what would have otherwise been dozens of separate small-to-medium dye batches into a single, massive, uninterrupted production run, the efficiency gains are both real and compounding.
Haglöfs’ internal production assessments place these efficiency figures at over a 50 percent reduction in water usage and at least a 20 percent reduction in energy consumption when compared directly to traditional piece-dyed black fabrics. While these are company-supplied figures rather than independently verified metrics, the underlying chemical and industrial logic is sound. Batch consolidation is a universally understood lever in industrial chemistry, meaning the efficiency gains are hardly surprising. What remains surprising to industry insiders is that no major brand undertook this collaborative step sooner.
Standard Issue Black enters full commercial production for the first time during Haglöfs’ Fall/Winter 2026 season, marking the critical transition from theoretical concept to industrial implementation.
The Buteo Mid II Jacket serves as the first commercially available product built entirely on this new universal standard. Deliberately, it is not a limited-edition concept piece meant only for exhibition. Eva Weiss, Haglöfs’ Head of Design and Research & Development, was explicit regarding the choice of vehicle: the Buteo is one of the brand’s higher-volume, mainstream styles.
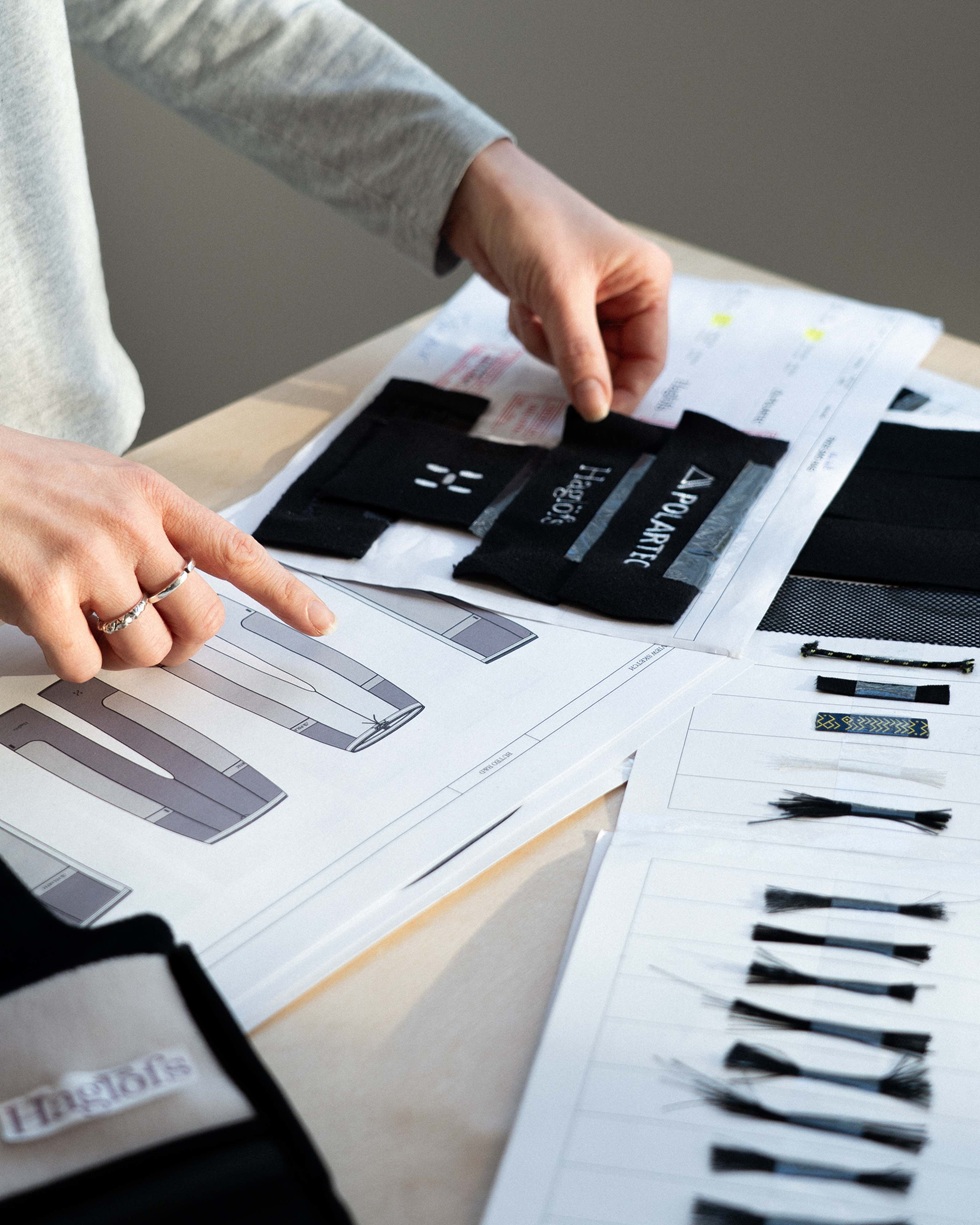
It is the kind of functional jacket that sells in significant quantities across global markets, which is precisely the point of the initiative. The true environmental case for Standard Issue Black only holds validity when applied at volume. Relegating the standard to a niche, limited-run collection would have merely been a symbolic demonstration; integrating it into a proven bestseller represents a fundamentally different kind of corporate statement.
The Creativity Question
The immediate objection that occurs to nearly every apparel designer encountering this concept is an obvious one: does standardization ultimately kill creative expression? If every outdoor brand utilizes the exact same shade of black, critics argue, everything on the retail floor will begin to look identical.
It is a reasonable concern for design teams whose job is brand differentiation. However, the color black has historically never been the primary vehicle through which outdoor brands truly differentiate themselves. True design differentiation lives in the cut, the technical construction, the specialized hardware, the broader colorway story, the technical fabric specifications, the fit, the trim details, the subtle logo placement, and the seasonal accent colors. Black has always served as the reliable, unchangeable background constant of technical apparel.
Eva Weiss addresses this directly, noting that standardization does not have to limit creative potential. Within the right operational framework, she explains, it actually provides designers with the freedom to collaborate in the same positive creative direction while driving a much larger collective impact. Having one clearly defined, universal black simplifies the overarching design process, leaving brands fully empowered to differentiate themselves through unique cuts, contrasting colors, and innovative functional details.
There is a historical parallel worth drawing within the outdoor equipment sector. The industry successfully standardized on a small number of zipper systems decades ago, to the point where the dominance of YKK hardware on a garment is entirely unremarkable to the consumer. Yet nobody seriously argues that the widespread standardization of zippers has ever stifled creativity in modern outerwear design. The standardization of a foundational, functional component simply freed up valuable design energy for the elements that genuinely matter to performance and style. Standard Issue Black makes the exact same functional argument regarding color.
Will Other Brands Follow?
What makes broader industry adoption genuinely uncertain is the outdoor sector’s long, complicated history with sustainability initiatives that are well-intentioned, carefully designed, and then quietly ignored by competing brands that were not initially involved in their creation.
The persistent hurdle of the green premium—the frustrating gap between what consumers say they value in surveys and what they are actually willing to pay at the cash register—has historically derailed more promising environmental ideas than any amount of regulatory pressure from governing bodies.
Standard Issue Black largely sidesteps that specific commercial question because it does not carry an inflated price tag. The core economics are neutral to positive, the environmental case is mathematically clear, and the only potential hurdle is the creative objection that may cause some legacy brands to hesitate.
What remains to be overcome is deep institutional inertia. It is the exact same organizational force that kept the broader textile industry running dozens of separate black dye processes for decades when the cleaner alternative was obvious. It is the same systemic resistance that emerging innovators are fighting across various sectors of material science. The global manufacturing machine keeps running smoothly because stopping it, even temporarily to retool, can be uncomfortable for corporate supply chains.
Standard Issue Black does not ask anyone to completely stop the industrial machine. It simply asks them to do less of the redundant work. Whether that request is straightforward enough to be answered by enough brands, at a high enough manufacturing volume, to make the standard mean something far beyond Haglöfs’ own product catalogue is the ultimate question the Black Capsule raised, and one that the Buteo Mid II is now beginning to answer.